

2ndhandyotaman
Member
I'm hoping to find some folks that are professional welders/fabricators who might be willing to take a look at the following pics and offer feedback/insite on what I'm getting wrong w/ my TIG welds.
I've just began using a TIG welder a few months ago after taking a very basic ( too basic IMHO) intro class at the local Maker Space. I try to practice at least a few hours every week. I can see that I;'m doing (many) things wrong by the look of the welds, I'm just not sure what it is that I'm getting wrong.
Todays practice session was using some .180 thick 1018 CRS , scraps left over from the water jet. ( scraps are free at the maker space, so it works for me !)
We have Miller 210 Syncrowave machines, I'm using DC TIG at 190 amps. ( using the 1 amp/.001 material thickness guideline) and 3/32 copper coated TIG wire. Tungsten is clean and ground to a nice point, no contamination.
When I was doing the lap joint, the puddle looked wet and looked like it was flowing nicely. When I stopped, I saw this mess. I can see where I wasn't even inside of the joint, and it looks like I was under cutting the top edge. Is this from too much heat?
The top pass doesn't look as bad, it was a butt joint.
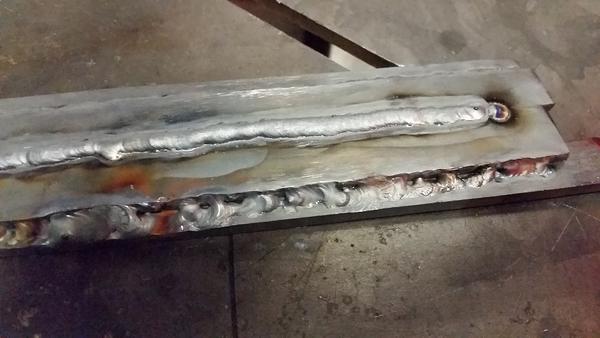
I started and stopped a few times on this pass. Same issue as above- some of the welds look too big and they undercut the edge of the material, or the joint looks like the puddle wasn't flowing properly.
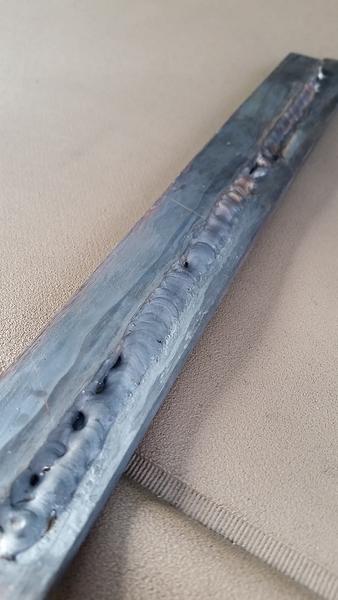
Last piece of the practice session. Overall, this was the best welds of the day and they still aren't all that good looking to me.
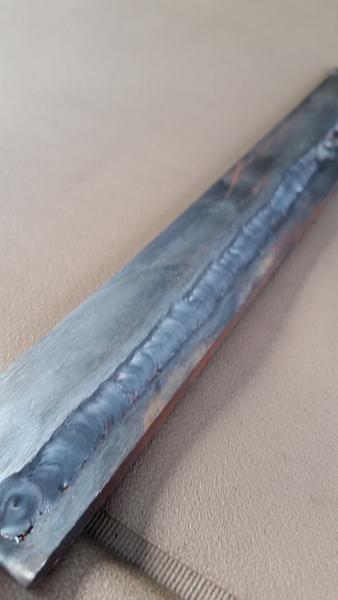
The weld looks too big, it cut into the edge of the material although it looks like the puddle actually did stay flowing this time. In each practice piece, I did the exact same thing in regards to starting/stopping the weld, used the same amperage settings and same filler rod. Obviously I'm doing something(s) very wrong, I just don't know what.. I'd welcome any feedback/ constructive criticisms. I want to get to the point of being able to show off the weld joints on square and round tubing when I build furniture.
I just started building very basic steel frame/hard maple coffee and end tables last year. I made a set for myself and one set for a friend that really wanted a set. I MIG'd everything and was ok with those welds. I just think that a properly laid TIG weld is something to be seen, not ground smooth and hidden under a layer of powder coat.
I've just began using a TIG welder a few months ago after taking a very basic ( too basic IMHO) intro class at the local Maker Space. I try to practice at least a few hours every week. I can see that I;'m doing (many) things wrong by the look of the welds, I'm just not sure what it is that I'm getting wrong.
Todays practice session was using some .180 thick 1018 CRS , scraps left over from the water jet. ( scraps are free at the maker space, so it works for me !)
We have Miller 210 Syncrowave machines, I'm using DC TIG at 190 amps. ( using the 1 amp/.001 material thickness guideline) and 3/32 copper coated TIG wire. Tungsten is clean and ground to a nice point, no contamination.
When I was doing the lap joint, the puddle looked wet and looked like it was flowing nicely. When I stopped, I saw this mess. I can see where I wasn't even inside of the joint, and it looks like I was under cutting the top edge. Is this from too much heat?
The top pass doesn't look as bad, it was a butt joint.
I started and stopped a few times on this pass. Same issue as above- some of the welds look too big and they undercut the edge of the material, or the joint looks like the puddle wasn't flowing properly.
Last piece of the practice session. Overall, this was the best welds of the day and they still aren't all that good looking to me.
The weld looks too big, it cut into the edge of the material although it looks like the puddle actually did stay flowing this time. In each practice piece, I did the exact same thing in regards to starting/stopping the weld, used the same amperage settings and same filler rod. Obviously I'm doing something(s) very wrong, I just don't know what.. I'd welcome any feedback/ constructive criticisms. I want to get to the point of being able to show off the weld joints on square and round tubing when I build furniture.
I just started building very basic steel frame/hard maple coffee and end tables last year. I made a set for myself and one set for a friend that really wanted a set. I MIG'd everything and was ok with those welds. I just think that a properly laid TIG weld is something to be seen, not ground smooth and hidden under a layer of powder coat.

