Welding Advice Please!

Antman

Elite Member
Hey guys!

I've always wanted to learn to weld and decided to take the plunge. Harbor Freight has this flux core welder on sale for less than $100:

Wire Welder - Save on this 90 Amp Flux Wire Welder

I realize it isn't the best out there, but the reviews are mostly positive for this unit. I'm not looking to fab a tube frame buggy or anything, just have some fun...

SO- today I started practicing some welds. As expected, they look like crap, LOL! It's gonna take a lot of practice for sure. I have been looking at videos online and trying to read up on the topic as much as possible. Which leads me to my question for all of you experienced welders:

Any advice?

What's a good place I can go- or literature I should buy- that can give me a solid start?

Machine setup tips?

Typical beginner mistakes?

Safety concerns? I have leather gloves and an auto-darkening shield so far...


Thank you in advance, I appreciate it!

Jeff
 
Last edited:
Register to hide this ad
Start by looking at a few videos on youtube. There are a lot of good videos there that will teach you a lot.

A few pointers... If it's slag you drag. Meaning, with a flux core welder drag the gun away from the weld while welding. If you're mig welding with gas you will push. Keep the gun at about a 45* angle and about 1/4-3/8 inch away from the material and do little squigglies until you start seeing a nice orange puddle and pull the gun away and let the puddle follow the gun. As far as wire speed and heat, you will have to play with that and learn your welder. If you're getting good penetration you should see nice heat marks near your beads. Start with some 1/8" thick material and expand out from there. 1/8" for me was the easiest to learn on. It's not so thin that you'll burn through it easily and its not so thick that you have to worry about over heating and warping the product.
 
Start by looking at a few videos on youtube. There are a lot of good videos there that will teach you a lot.

A few pointers... If it's slag you drag. Meaning, with a flux core welder drag the gun away from the weld while welding. If you're mig welding with gas you will push. Keep the gun at about a 45* angle and about 1/4-3/8 inch away from the material and do little squigglies until you start seeing a nice orange puddle and pull the gun away and let the puddle follow the gun. As far as wire speed and heat, you will have to play with that and learn your welder. If you're getting good penetration you should see nice heat marks near your beads. Start with some 1/8" thick material and expand out from there. 1/8" for me was the easiest to learn on. It's not so thin that you'll burn through it easily and its not so thick that you have to worry about over heating and warping the product.

Awesome! I'm having trouble seeing the puddle- exactly where it is. I know that sounds stupid, but I thought I would get a clearer picture of what was going on.
Basically I feel like I'm just building up material on top, and not actually allowing the puddle to follow the gun... One of my welds so far seems pretty good though!
 
Awesome! I'm having trouble seeing the puddle- exactly where it is. I know that sounds stupid, but I thought I would get a clearer picture of what was going on.
Basically I feel like I'm just building up material on top, and not actually allowing the puddle to follow the gun... One of my welds so far seems pretty good though!

What helmet do you have and what do you have it set at? I would have trouble seeing the puddle when I had the helmet set too dark.
 
I had that welder. My welds got better when I pitched the crappy HF wire and replaced it with decent Lincoln flux core (Lowes has it). My welds got even better yet when I pitched the HF welder completely and replaced it with a Lincoln :D.

1) Prep the metal well. Flap wheel it down to bare metal, then degrease it with some acetone (don't use brake cleaner, that'll turn into poison gas if it's still on the metal when you start welding). Clean metal is critical.

2) Make a good ground. Sometimes that means flap wheeling where you're going to attach the ground strap. It also means try not to use extension cords if you can help it, and make sure the wall socket you're using for power has a good ground connection. A solid ground is critical.

3) Make a good puddle. Practice making a puddle with the weld, you'll know it once you see it. Getting a good puddle is critical to getting good penetration, and penetration of the weld is what you need - remember that you aren't gluing your metal together, you're fusing it, there's a huge difference. Once you can make a good puddle, practice moving it along your weld.

You'll know you've got the right amperage and speed when you're making a frying eggs sound and you can see your puddle develop within a couple seconds. If it's popping and crackling and spitting everywhere, then one of the above is off. Once you've made a weld, get out the hammer and see if you can bust it apart - if you can, then you didn't penetrate and one of the above is off.

There's lots of good videos on youtube, I really like this one: How to Weld, Part 1 - YouTube.
 
Jeff, keep in mind I am not too experienced in welding AT ALL, but flux core is probably one of the key issues why your beads look like shiat. Anyway to convert that welder over to a MIG setup and get some solid core wire? I used to own a cheapo flux core welder and almost gave up on welding all together because everything I did looked like crap, lol.

Anyways, maybe if you post some pictures, the more experienced welders would be able to help you troubleshoot the issue. From what you are saying it sounds like you're not getting enough penetration so maybe crank up the heat a notch? If the puddle is sitting on top of the base metal, then it's not really melting into the base metal enough to achieve a proper umm..."bond".

If you're having trouble seeing the puddle, you might be able to change the shade level on that helmet of yours?
 
It's from harbor freight as well-
Welding Helmet - Save on this Auto-Darkening Welding Helmet


I figured the darker the better- ha! I had it turned almost all the way up. Rookie! I'll adjust that and see what happens..

Ah, that's your problem. Turn that down. Don't worry about burning your eyes. Any decent, modern auto-darkening helmet will protect you from IR/UV even when the helmet isn't darkened. Turn it down until you can see the puddle, and prepare to be amazed lol.

Also, I started out on a cheap auto-darkening helmet like that too. Sometimes it wouldn't darken on out-of-position welds, so I bought a nice Lincoln one, and I haven't had a problem since. But for starting out, that helmet should be fine.
 
Number one reccomendation for the harbor freight welder is get a good quality flux core wire. You can pick up a spool of Lincoln flux core wire at Home depot for $12, and it drastically changes the way the welder feels and works. Aside from that, keep practicing. A lot of welding is feel and gaining fine control over the gun in order to maintain and move the puddle along, which can only come with time spent welding. Keep at it, and youll quickly see yourself improve.
 
Harbor freight is your first problem though. I have never used their welders, I have always been more of a miller or Hobart (made by miller) fan. But as said above, make sure your ground is solid, metal is clean and you have good wire. Those three alone will eliminate a LOT of frustrations. I am not an expert welder but I do have a bit of welding time under my belt and once in a while I'll get cocky and get my ass kicked by trying to weld dirty metals.

Anything else is gained by practice and experience.

Try to make a few beads and post some pictures. We can help tell you what you're doing wrong by the look of your work.

***************************

Another thing that hasn't been covered yet... SAFETY!!!

DO NOT USE CHEMICALS when you're cleaning the metal. The last thing you want to do is use a chemical to clean the metal then drag electricity over the top of it and create a small and possibly fatal smoke cloud from burning chemicals. Use a flap wheel or wire brush to clean your metals.

If your welding helmet isn't cutting the mustard, spend the money and get a good one. A good helmet is a lot cheaper than a second set of eye balls. Consider this a part of a life support system.

Never weld in shorts and tennis shoes. I learned this one the hard way and had a nice orange ball of melted steel eat through my shoe and tickle my foot. It didn't feel good. Get a decent welders jacket, gloves, and at a minimum some jeans and leather boots. Once you're better at positioning yourself around your work then maybe you will feel more comfortable wearing less protective clothing.
 
I've got that helmet and had that welder. In short it was fun to have and it paid for itself just doing little projects here and there. I ran Lincoln wire through it and accepted the machine for what it was.

One thing I liked about it is that it was small and portable. None of my stuff is structural or works of art so I took my time. If something needed some grinding and multiple passes I went for it.

In the end you'll get only meh results with a 110v machine. I have a Lincoln 110 MIG machine now and it still works for me. Most guys won't touch these but for me it's what I have, use and like. You need a good technique and understanding of what you need to do and what is being done. It's not just melting wire in a crack.

I always used the high setting as the low doesn't get anywhere near the penetration you need even for light pieces. Flux core, even at low, will blow holes in thin stuff, this is where MIG (gas) is necessary. Your machine isn't a gas machine so just run with what you've got.

One thing I've noticed with my Lincoln is that things need to be really clean. Like bare bare metal whereas the HF unit would basically burn through most mill scale, light paint and rust. The less prep you do on the metal the dirtier and weaker the weld will be so take you time, even for practice. After a couple of 1lb spools I bought the 8 or 10 pound one and refilled the smaller spools for cost savings. It's a PITA but was worth it since a 10 lb spool is the cost of the machine. I paid $80 for my 90 amp, new.

For the helmet I always have it set to 11 and have done well. For me I see best when I'm out in the sunlight. It allows me to see what I'm doing before it starts going and the fresh air is good to remove the smoke and fumes.

My HF unit bit the dust because of the drive roller for the wire. Keep the lid on, wire clean and every once in awhile remove the wire from the wand and blow the wire casing clean with compressed air.
 
Last edited:
I've got the Lincoln 110v too, a Weldpak 100 I think it's called. If I'm careful and take my time, it'll just barely do 3/16ths. I think it's enough for a hobby welder.

20131014_160341_zps7921353d.jpg~original
 
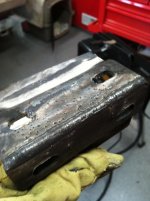
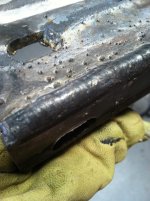
Well guys- thanks for the good advice! I had a little time to practice with some scrap and I think I actually made a decent weld here! It's strong too, the bracket bent when I hammered on it in a vice- weld held great.

CLEAN metal and setting that helmet correctly helped a lot. What do you guys think?


IMG_3544.jpg

IMG_3545.jpg


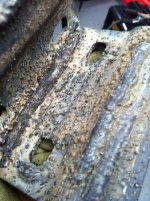
And now the other side, LOL. I don't know exactly what happened here, but it seems like the inside corner weld was just sitting on top? The beads I laid flat also had a LOT of splatter. I'm still working through that cheap H/F flux core wire, so maybe that's it? I dunno- it's still a learning game at this point (and will be for a few years I think...) HAHA!


IMG_3546.jpg


Criticism welcome! Thanks again- Jeff
 

Attachments

  • IMG_3544.jpg
    IMG_3544.jpg
    127.5 KB · Views: 787
  • IMG_3545.jpg
    IMG_3545.jpg
    135.6 KB · Views: 792
  • IMG_3546.jpg
    IMG_3546.jpg
    139.4 KB · Views: 770
For a flux weld, it looks REALLY good!!

The first pic about 1/3 of the way through it looks like you sped up a little bit. Consistency is key. Keep a steady speed of movement and distance away from your material. Overall it looks awesome!

The lower pics, the additional splatter may be from too great of a distance between your gun and material. You will have some splatter that you cannot avoid because it's the nature of a flux welder.
 
For a flux weld, it looks REALLY good!!

The first pic about 1/3 of the way through it looks like you sped up a little bit. Consistency is key. Keep a steady speed of movement and distance away from your material. Overall it looks awesome!

The lower pics, the additional splatter may be from too great of a distance between your gun and material. You will have some splatter that you cannot avoid because it's the nature of a flux welder.


Thanks man! The advice in this thread really helped- especially about making a pool and watching it follow the gun. It helps to have some clue at least LOL!
 
Wow Jeff, looking GOOD! Way better than what I've ever accomplished with flux core. I guess it's official, I need to stop blaming the welder (machine) and start blaming the welder (me) :(

Can't wait to see what kind of mods you can whip out now that you're equipped to weld, lol.
 

Members online

Forum statistics

Threads
278,308
Messages
3,554,059
Members
248,016
Latest member
Advally Service

Trending content

Back
Top